Key takeaways
- Threading capacity: Most trades work lives between 1/8″ and 2″ NPT. If you handle 2-1/2″–4″ mains or sprinkler lines, you need a machine rated for it — forcing a 2″ machine beyond its rating burns out gears.
- Motor power: Corded universal motors in the 1/2–1-3/4 HP range dominate. Higher horsepower matters less than torque at low RPM for large diameters.
- Die-head changeover: Quick-opening die heads save real time when alternating between 1/2″ and 2″ pipe. Bolt-on die heads on budget machines can take five minutes per swap.
- Portability: A handheld power drive plus tripod stand weighs under 30 lbs; a shop machine on a stand can exceed 500 lbs.
- Oil management: Cutting oil extends die life dramatically. Built-in recirculating oil systems filter and reuse oil; machines without them need manual brushing, which wastes oil and makes a mess.
- Chuck and gripping: Rear chucking capability lets you thread close to pipe ends and handle short nipples — a big deal for repair work.
- Cutting accuracy: A rigid carriage and quality dies produce threads that gauge correctly the first time, avoiding rework on pressurized systems.
For most working plumbers in 2026, the best pipe threading machines are the RIDGID 535 for shop work, the RIDGID 700 Power Pony for mobile jobs, and the RIDGID 1224 when you need capacity beyond 4-inch pipe — the right pick depends on whether you’re threading a few nipples a week or cutting pipe all day.
Our top picks


As an Amazon Associate we earn from qualifying purchases at no extra cost to you. Ratings are shown as listed on Amazon.
What Actually Matters When Choosing a Pipe Threader
Spec sheets list dozens of numbers, but seven factors decide whether a machine fits your work:
- Threading capacity: Most trades work lives between 1/8″ and 2″ NPT. If you handle 2-1/2″–4″ mains or sprinkler lines, you need a machine rated for it — forcing a 2″ machine beyond its rating burns out gears.
- Motor power: Corded universal motors in the 1/2–1-3/4 HP range dominate. Higher horsepower matters less than torque at low RPM for large diameters.
- Die-head changeover: Quick-opening die heads save real time when alternating between 1/2″ and 2″ pipe. Bolt-on die heads on budget machines can take five minutes per swap.
- Portability: A handheld power drive plus tripod stand weighs under 30 lbs; a shop machine on a stand can exceed 500 lbs.
- Oil management: Cutting oil extends die life dramatically. Built-in recirculating oil systems filter and reuse oil; machines without them need manual brushing, which wastes oil and makes a mess.
- Chuck and gripping: Rear chucking capability lets you thread close to pipe ends and handle short nipples — a big deal for repair work.
- Cutting accuracy: A rigid carriage and quality dies produce threads that gauge correctly the first time, avoiding rework on pressurized systems.
Best Pipe Threading Machines by Situation
Best Shop Workhorse: RIDGID 535
The 535 has been the industry benchmark for decades, and the current version keeps that position. It threads 1/8″–2″ pipe standard (up to 4″ with the 141 geared threader accessory), runs a 1/2 HP motor, and includes an integral recirculating oil system that filters chips out of the cutting fluid. The hammer-type chuck grips with minimal slip, and quick-opening die heads swap in seconds. At roughly 260 lbs on a stand, it stays in one place — that’s the point.
Best for Mobile Plumbing: RIDGID 700 Power Pony
The 700 is a handheld power drive that accepts 12-R die heads for 1/8″–2″ work. Paired with a chain vise or the optional support arm, it weighs around 25 lbs and fits in a van easily. For service plumbers threading a few nipples on-site, it eliminates carrying a 300-lb machine through a client’s building. The trade-off: no built-in oiling, so you brush oil on manually, and large-diameter threads take patience.
Best High-Capacity Option: RIDGID 1224
When the job involves 2-1/2″–4″ pipe regularly — sprinkler systems, commercial gas mains, industrial work — the 1224 threads up to 4″ standard (6″ with accessories) using a more powerful motor and a heavier carriage. It runs both 1/2″–2″ and 2-1/2″–4″ die heads without adapters, which matters on mixed-diameter jobs.
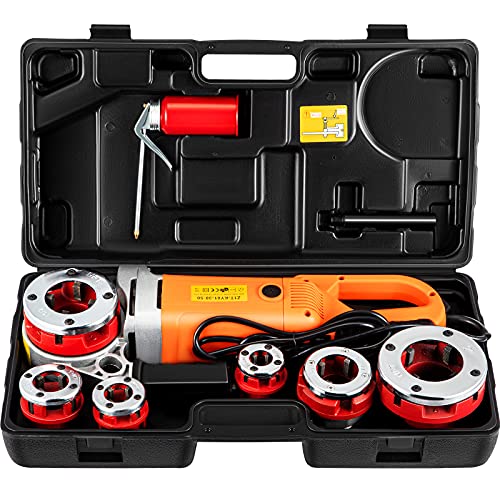
Best Budget Shop Machine: Steel Dragon Tools / VEVOR-style Electric Threaders
Import machines in the $500–$1,200 range thread 1/2″–2″ pipe acceptably for low-volume shops and maintenance departments. Expect heavier die-head changeovers, noisier gearboxes, and shorter die life. They’re a reasonable entry point — but budget for replacement dies and check that die heads follow the common RIDGID-compatible pattern so consumables stay easy to source.
Spec Comparison at a Glance
| Machine | Capacity | Motor | Weight | Oil System | Typical Price Range |
|---|---|---|---|---|---|
| RIDGID 535 | 1/8″–2″ (4″ w/ 141) | 1/2 HP universal | ~260 lbs w/ stand | Built-in recirculating | $3,500–$5,000 |
| RIDGID 1224 | 1/4″–4″ (6″ w/ accessories) | 1-1/2 HP induction | ~500 lbs w/ stand | Built-in recirculating | $6,000–$9,000 |
| RIDGID 700 Power Pony | 1/8″–2″ | ~1/2 HP handheld | ~25 lbs | None (manual brush) | $1,800–$2,600 |
| Import 2″ electric threader | 1/2″–2″ | ~1/2–1 HP | ~150–200 lbs | Usually drip tray only | $500–$1,200 |
Decision Matrix: Match the Machine to Your Work
| Your situation | Recommended pick | Why |
|---|---|---|
| Service plumber, 1–10 threads per job, works on-site | RIDGID 700 + chain vise | Carry-in portability beats thread speed at low volume |
| Shop plumbing/heating contractor, daily threading | RIDGID 535 | Oil system and quick die heads pay back in labor savings |
| Sprinkler or commercial pipefitter | RIDGID 1224 | 4″ capacity without slowing down on 2″ work |
| Facility maintenance, occasional repairs, tight budget | Import 2″ threader | Low cost per use; RIDGID-pattern dies keep consumables cheap |
| One-time project or rare use | Rental (typically $60–$120/day) | Break-even vs. a 535 is roughly 40+ rental days |
Ownership Realities Listings Don’t Mention
Dies are your real consumable cost. A set of quality die heads runs $150–$400 per size and lasts thousands of threads with proper oiling — or hundreds without. Always thread with cutting oil, never dry, and never reuse oil contaminated with metal chips unfiltered.
What wears first: die teeth, chuck jaws, and — on machines with recirculating oilers — the pump intake screen. Clean the chip tray and screen weekly under daily use.
Common mistakes: setting the die head to the wrong size before engaging (check the size bar), cutting threads longer than standard NPT engagement depth (roughly 0.8–1.0″ for 1/2″–1″ pipe), and letting pipe whip because it wasn’t supported on long lengths — use a pipe stand on the outboard end.
Runtime math: a 535 cuts a 3/4″ NPT thread in roughly 15–25 seconds including oil flow warm-up; a handheld 700 takes about twice that plus manual oiling. At 30+ threads a day, the shop machine saves close to an hour of labor daily — enough to justify the price gap within a year for busy contractors.
Setup Basics for Accurate Threads
- Ream the pipe end first — burrs deflect the die and cause cross-threading.
- Set the die head size scale to match the pipe; verify with a thread gauge on the first cut of the day.
- Apply oil before the dies contact the pipe and keep flow steady through the cut.
- Let the die head ride at its own pace; forcing the carriage produces tapered or torn threads.
- Back off, clean the chips, and test-fit with a fitting or gauge before removing the pipe.
Frequently Asked Questions
Can a handheld power drive replace a shop machine?
For low volume, yes — a 700 with 12-R die heads produces identical NPT threads. It loses on speed, oiling convenience, and comfort when threading dozens of pieces.
Do import machines use standard dies?
Many use die heads patterned after RIDGID’s 11-R/00-R style, but confirm before buying — proprietary dies lock you into one supplier.
Is NPT threading different from BSPT?
Yes — different taper and thread form. Die heads are not interchangeable; buy dies matching the standard your fittings use.
The pattern across all of this is simple: volume and pipe size pick the machine, oil discipline and die quality decide your thread accuracy, and matching the tool to your daily workload — not the biggest spec sheet — is what makes the investment pay off.